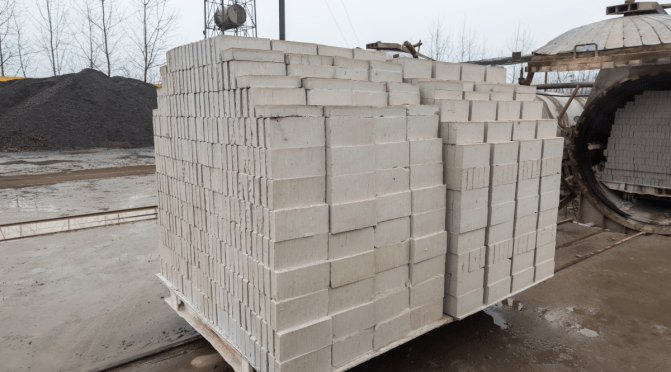
AAC Blocks or Autoclaved Aerated Concrete Blocks are a lightweight, load-bearing, a durable, eco-sensitive, and economical alternative for conventional bricks. AAC Blocks can be customised to satisfy dimensional requirements. When compared to concrete,wood ,brick and stone AAC block possess excellent insulation, fire-resistant, and thermal resistant properties. AAC block can enhance construction speed and reduce costs.
AAC BLOCKS LAYING
AAC Blocks Manufacturing
AAC block constitute 80% voids and hence it is lightweight and easy to handle. They are manufactured using easily available materials. The ingredients include sand, fly ash, lime, cement, gypsum, and aluminum powder. The manufacturing process is clean and does not emit any hazardous chemicals. Major raw materials used for AAC block manufacturing are industrial wastes like fly ash and gypsum. The manufacturing process is energy efficient eco-friendly certified green building materials.
Ingredients of AAC blocks
The main ingredients of AAC blocks are Fly ash, Sand, Cement, Lime, Gypsum, water, and aluminum powder. Aluminum powder is used as a foaming agent.
Cement used for AAC block manufacturing is OPC 43 or OPC 53 grade cement and is used as a binding material.
Fly ash is an industrial waste from power plants. The density ranges from 600kg/cm3 to 1400kg/cm3. The presence of fly ash is responsible for imparting insulation and fire-resistant properties of AAC blocks.
The lime is obtained by grinding limestone in the block manufacturing factory or outsourcing as lime powder.
Aluminum is used as a foaming agent and is responsible for the development of voids inside the blocks.
Gypsum is an industrial waste generated from fertiliser plants and is abundantly available.
AAC Blocks manufacturing process
The manufacturing process of AAC blocks is associated with a series of operations starting from, feeding of ingredients to the stacking of blocks. Every stage is associated with strict manufacturing quality guidelines for ensuring requisite strength and density. AAC block manufacturing processes are broadly classified as follows.
Raw material preparation
Dosing & mixing
Moulding, rising and pre-curing
De-moulding and Wire cutting
Autoclaving
Raw material Preparation
The basic ingredients required for AAC block manufacturing are fly ash or sand. Fly ash is abundantly available as industrial waste from power plants. Hence fly ash is used for manufacturing AAC blocks. It is mixed with water to form fly ash slurry which is stored in containers for the next stage of operation.
Dosing and mixing
The fly ash slurry is stored in a container which is connected to a mixing drum. All other ingredients like lime powder, gypsum, and cement are stored in different storage containers and are fed into the mixing drum using screw conveyors. Automatic feeding systems are attached to each storage container to ensure correct ingredient proportions. The proportioned ingredients are simultaneously fed to a mixing drum where it is mixed thoroughly. Aluminum dosing is done through a feeding attachment and is controlled according to the requirement. The ingredients are thoroughly mixed and ready to be poured into the moulds.
MIXING DRUM
Moulding, rising and Pre-curing
The casting of AAC blocks is done in moulds. The moulds are cleaned and coated with oil to avoid any sticking of the ingredients on the surfaces of the mould which in turn can hamper the surface finish of blocks. Already mixed slurry is poured into the oiled moulds. Inside the moulds, the aluminum reacts with calcium hydroxide (lime) and water and produces a lot of unconnected hydrogen bubbles and expands the slurry. The expansion is almost twice that of the original volume. This process is called rising. These hydrogen bubble spaces are responsible for the lightweight characteristics of AAC blocks. The process of rising is followed by de-moulding and cutting the blocks. The cutting of the blocks into the required sizes requires some strength for the cube. For that, the mould is allowed to settle and cure for a while just enough for the wire cutting process. The pre-curing time can be anywhere between 1-3 hours or more depending on weather conditions. This can be done by indirect heating also. After the pre-curing process, the green cake is strong enough for a wire cut.
De-moulding and Wire cutting
The pre-cured moulds are carried to the cutting area. The moulds are removed and the green cake is wire cut as per the required sizes. The wire cutting process is done in two stages. The first stage is a vertical cut and the second stage is a horizontal cut. De-moulding and cutting give the dimensional perfection and finish of the AAC blocks. This process has to be done with utmost care or else rejection may happen.
WIRE CUTTING OF AAC BLOCKS
Autoclaving of AAC blocks
The final process of manufacturing is autoclaving. The wire cut blocks are transported to an autoclaved chamber where is heated to the required temperature. This process gives the desired durability and structural stability to AAC blocks. The baking is done for about 8-12 hours at a temperature of around 180 degrees. The temperature and period of heating determine the grade of the materials. Curing in an autoclave reduces drying shrinkage.The autoclave curing process requires more energy and a more expensive kiln, but it can produce blocks in less time.
The blocks are stacked on pellets on completion of autoclaving process for transporting to the required destinations. All quality tests are conducted in the factory itself.
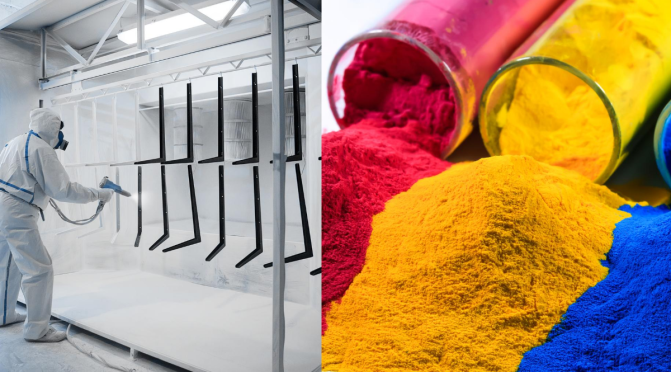
The powder coating process is a method of spraying electrostatically charged dry powder over the material surface. The powder coating process is also known as the electrostatic spray deposition process. The dry powder constitutes a combination of finely ground pigments and resins. Powder coating was introduced in the late 1980 s and is being extensively used in the industrial, commercial, and household applications. This process provides a smooth, durable, decorative, and a corrosion-resistant coating.
POWDER COATING PROCESS
Difference between Powder coating process and Polyester Powder coating
A lot of confusion is prevailing between the terms, “Powder Coating” and “Polyester powder” coating. Powder coating is the method of application of electrostatically charged dry powder to the material to be coated. Powder coating can be applied on any surface. However, the powder coating ingredients differs with material types and the environment where it is used. The most popular powder coating types are Epoxy Powder Coating, Polyester Powder Coating, and Hybrid Powder Coatings.
Polyester powder coatings preferred in applications are classified into TGIC Polyester coating and Urethane polyester coating. For aluminium extrusions, TGIC Polyester coating is preferred due to there low temperature curing properties.
Powder coating process is broadly classified into three important stages.
Surface preparation
Powder coating process
Curing process
Surface Preparation
The durability and serviceability of a coating depend on the quality of surface preparation. Surface preparation is essential to remove the dirt, grease, and other impurities from the material surface. The cleaning process includes various stages of cleaning, rinsing, etching, blasting, and drying, etc. The surface preparation stages are as follows.
Chemical cleaning
Conversion coating
Chemical cleaning
The chemical cleaning process uses mild alkalies(caustic soda), acids, and detergents for cleaning. The cleaning process is followed by rinsing with hot water, steam, detergent, etc. However, the type of acid/alkali cleaners depends on the material type to be coated. For example, aluminium is sensitive to acid attacks and requires mild alkaline cleaners. Rinsing with nitric acid done on anodised surfaces. On completion of the cleaning process, the surface feels smooth and free from grease, oil, impurities, etc
REMOVING MATERIALS FROM OVEN
b) Conversion coating
A conversion coating is applied on the surface to enable strong adhesion with powder coating. The chemical solutions for conversion coating are selected based on the type of material to be coated. For aluminium surfaces, the conversion coating is applied for a surface with strong adhesive nature and to arrest the progress of oxidation before powder coating.
For aluminium surfaces, conversion coating uses chromatic or phosphate solutions. In mild steel Zinc phosphate/ iron phosphate solutions are used. After completing the conversion coating, the coated material is cleaned in rinsing tanks. The final rinse is done using simonized water. The rinsing process removes chemical salts and other residues from the surface of the material that can trigger corrosion and can affect the coating adhesion properties.
On completion of the conversion coating, the material is dried in a drying oven to remove any possible moisture before application of the coating.
Powder coating process-Types
Once the drying process is over, the clean and dry material from the drying oven is shifted to a powder coating booth for powder coating. The powder coating application is commonly done in two methods based on the type of material and environment where it is used.
Electrostatic deposition
Fludized bed powder coating
Electrostatic deposition
In Electrostatic spray deposition or ESD method of powder coating, the finely ground powder is sprayed by a gun to the material. The entire system constitutes a spray booth, a powder feeder, an electrostatic spray gun, and a power unit. For the ESD process of powder coating, a finely ground resin and pigment powder are charged inside a gun. The material to be coated is grounded/earthed to provide an opposite charge. The electrically charged particles from the gun are sprayed on to the earthed material. The powder on leaving the gun gets attracted to the earthed parts due to electrostatic attraction. In this process, areas that are not even in line with the gun also get attracted to the material to be coated. The powder will continue to stick on the surface as long as it is grounded/earthed. The thickness of the coatings depends on the type of environment the part will be used in. Any powder left after the coating is reclaimed and reused.
POWDER COATED MATERIALS
Fluidized bed powder coating process
In the Electrostatic deposition process, the powder coating material is electrostatically sprayed and adhered to the surface. But in the case of fluidized bed powder coating, preheated parts are dipped to the powder material within a fluidized bed. There is also an alternative option called electrostatic fluidized bed powder coating, which generates a cloud of electrically charged powder particles above the fluidized bed through which the part to be coated is passed.
Curing of coated materials
The coated materials are co to an oven, where the painting process gets completed by ‘curing’ the particles. The oven heats the metal to about 200°C. The high temperature first fuses and melts the powder particles, allowing them to flow together to form a film and then cures the resin system in the film to form a smooth surface. Other additives within the powder formulation make them anchored to the conversion coating, developing a cohesive structure. After the curing oven, sections are transported to a cooling station, inspected, packed, and dispatched.
CURING BOOTH FOR POWDER COATING
Advantages of powder coatings process over liquid coatings
The wet painting system was the most common and traditional coating method. In this method, water-based or solvent-based paint is sprayed or painted to the material surface. Many concerns or issues associated with liquid paints are eliminated or minimised with the powder coating process. The advantages of powder coating over wet paint are listed below.
Resistance to corrosion and chemicals
Powder coatings are more durable and more resistant to corrosion, chemicals, weather, etc than liquid coatings. Powder coating provides wear, scratch-free, and abrasion-resistant coatings in comparison with liquid paints. The application process of powder coating is thermal bonding which provides a uniform, smooth, and even coating. The colours always look fresh and bright and give a refreshing look than liquid paints.
Color choice
Powder coatings offer an unlimited range of colours, finishes, textures, which is not achievable through any type of conventional liquid coating method. Powder coating can match the colour scheme of any object/structure. The enormous choice of colours and textures ranging from matt, glossy, and textured to metallic finishes makes powder coating one of the most preferred coating choices. Powder coating can be used as a protective coating as well as decorative applications.
POWDER COATING COLOURS
Durability of powder coating
Powder coatings are long-lasting and durable than any other liquid coatings. Powder coatings offer high resistance to impact, moisture, chemicals, wear, and abrasion compared to any other liquid coatings. They can also protect the materials against possible scratches occurring during the fabrication and fixing of the material and can be used in high traffic areas.
Environmental friendly
The liquid coatings emit VOC s (volatile organic compounds) due to the presence of solvents and cause serious environmental issues. Powder coating is free of any solvents and does not emit any VOCs and is thereby considered a green product. Moreover, the powder coating process does not create any hazardous waste that needs disposal. Any waste powder left after the coating is reclaimed and used. Powder coating is considered an environmentally friendly alternative to liquid coatings and thereby extensively used for green building-related projects.
Operational cost of powder coating
Powder coating is an economic option when compared with other organic finishes/ liquid painting methods. The powder coating application can be done with minimal training and supervision and thereby can reduce costs related to labour and operations. Powders left after the coating is recycled and reused. Fewer energy costs, reduced disposal costs, and low reject costs makes powder coating an economical option. Powder coating also has a longer life span when compared to other coatings and this can be another value addition in terms of money.
Safety
Liquid paints are flammable, carcinogenic, and full of volatile organic compounds and are harmful to the environment as well as the workers involved in the process, if not handled properly. Powder coating consists of solids and no solvents and hence is not harmful to persons handling it. Moreover, powder coatings possess good fire rating qualities in comparison with other liquid coatings.
Disadvantages of powder coating process
Thin coatings are difficult to produce
Powder coatings are 100% solid and because of this, even with a minimum amount of application, the initial thickness is formed. Moreover, it does not contain any volatile organic compounds. This makes it impossible to have thicknesses of less than 25 microns. Whereas in liquid paint, we have paint thinner and it is possible to have a lower percentage of solids, the film thickness can even be limited to 10 microns.
Failure of coating on exposed to atmosphere
On exposure to extreme atmospheric conditions like sunlight, heat, humidity, etc powder coating tends to fail, crack, and peel off. Hence not preferred for external applications involving exposure to extreme atmospheric conditions.
Color change after application
The production process and blending of powder coatings are carried out in a molten form. Hence it is not possible to change the color after production. Whereas in liquid paint we can change the color in all the stages, even when applying the paint, by adding stainers and pigments.
Size of coating material
The spray equipment and method of application of powder coatings confine the coating application to spray chambers only. Substrates must be charged and on completion of the coating. The materials have to be transferred to an oven where the curing process involving a temperature up to 200 degrees is done. Considering these conditions, it is not possible to coat and cure large substrates.
Oven curing
Powder coatings only dry and cure in temperatures above 180 degrees. Whereas liquid paints are varied and could dry up even in room temperature.
Control of material quantity and smoothness
Powder coating offers less control over the speed and amount of powder coating applied. The smoothness of the coating cannot be controlled as it is happening inside the oven.
Start up costs
The start up costs are high for powder coatings. Requires skilled workers for coating and operation of the plant.
After considering the limitations and advantages of powder coatings, and the selected product to be coated, you can evaluate whether coating metals with liquid paint or powder is more suitable.
Uses of powder coating process
Powder coating process is being used for a wide range of applications ranging from household , commercial, industrial ,automobile sectors.
Appliances
Powder coating is used for appliances like stoves, refrigerators, washers, dryers, dishwashers, air conditioners, water heaters, microwave ovens, and many other areas.
POWDER COATED HOUSE HOLD APPLIANCES
Automotive
Powder coating is used often in the automotive industry for engine parts and componets. It is also used by major auto brands as a clear top coat for increasing protection
Commercial Buildings and Offices
Powder coating is used for doors, windows, partions, roofing, cladding etc for residential buildings, commercial buiding etc.
Everywhere you look there are various building and highway projects which use powder coating as well – guardrails, light poles, fencing, posts, and signs are a few examples.
ALUMINIUM DOORS AND WINDOWS
Normal Daily Products
Many daily products are being powder coated to increase the quality of finishes. These products include antennas, lighting fixtures, and electrical elements. Farm equipment and tractors use powder coating. Fitness industries use powder coating on golf cards, golf clubs, ski poles, bicycles, snowmobiles, and other different types of exercise equipment.
Powder coating is also used for supermarkets, stores, malls etc . Every where around us we can see a material using powder coating.
Aluminium Anodising is an electrochemical process done on aluminium to increase the thickness of thin natural oxide coating and thereby enhance its corrosion properties. In our previous article Properties of Aluminium, the reasons behind applying a coating are described in detail. The anodic layer is non-conductive and acts as an insulation against electricity, sound, and heat. Aluminium anodising can increase the aesthetic look, absorb wear and tear and provide requisite durability against possible scratches occurred during handling, fabrication, and erection.
What is Aluminium Anodising ?
Anodising is an electrochemical process that transforms the metal surface into a decorative, durable, and anti corrosive anodic oxide finish. The Anodising process is conducted by passing an electric current through an electrolyte with aluminium to be coated as an anode. The oxygen ions released from the electrolyte get deposited on the surface of the object/anode. Oxygen reacts with aluminium to produce aluminium oxide. The thickness of Anodising ranges from 4 microns to 30 microns or some times more.
ANODISING TANK
Aluminium Anodising Process
The process of anodising is divided into stages depending upon t
Pre-treatment
The products to be anodised are cleaned in acid or alkali solutions to remove the dirt, grease, and other impurities from the surface. The pre-treatment method depends on the types of finish to be applied. The material is de-oxidised in an acidic solution to remove the natural oxide film.
Etching
Etching involves the removal of some parts of aluminium from the surface. This can be done using alkali or acid according to the finish coat type and texture. For satin finishes and precision parts light etching is done using alkali where minimum etching is done just enough to remove the natural oxide film. The alkaline solution used for light etching is Sodium Hydroxide. For non-precision parts and architectural extrusions, minor scratches and dye markings will be visible. Hence etching is done by treating in a concentrated mixture of phosphoric and nitric acids.
Etching process of aluminium
Brightening
Brightening is a micro level treatment done on the aluminium surface by chemical or eletrochemical means. This is done to level up the undulations. This provides a high lustre on the surface for receiving the coatings
Aluminium Anodising
The aluminium part to be anodised is submerged in an electrolyte solution. The electrolyte used in this process is sulphuric acid. The positive charge is applied to the submerged aluminium which acts as an anode and negative charge is applied to the plates suspended in the electrolyte. High voltage direct current is passed through the electrolyte constituting positive and negative ions. The electric current in the circuit causes positive ions to get attracted to the negative plates, and negative ions to flock to the positive aluminium anode.
Anodising aluminium in an electrolyte
Formation of barrier layer
The aluminium combines with the negatively charged oxygen ions to create aluminium oxide. This process develops a metal oxide film on the surface of aluminium that is treated. The layer quality can be adjusted with the concentration of solution and temperature.This is called a barrier layer, a defence against further chemical reactions at those spots.
FORMATION OF BARRIER LAYER
As current continues to be applied, the relatively weak and reactive areas of the pores will continue to penetrate deeper into the substrate, forming a series of column-like hollow structures. At this point the surface is porous and attracts dirt and other substances. Colour can be added at this stage.
SEQUENCE OF PORES FORMATION DURING ANODISING
For typical non-hard coatings, the depth can be up to 10 microns. Once this level is reached, and if no colour is needed, the process is stopped.
Sealing process
The final stage is sealing of pores and the process involves in dipping in a de-ionised water rinsing.
The coating can withstand chemical attack, scratch resistant and have a hardness index of 9 out of 10 in Mohs Hardness scale , means second only to diamond.
Application of colour
As mentioned above the barrier layer is porous like what is shown in the figure. At this stage we can go application of colour. The pigments fills the porous.
The pigment fills all the empty pores up to the surface, where it’s then permanently sealed off. That’s why anodised colours are so durable – they can’t be scratched off from the surface because in fact the colours are deep down and can only be removed by grinding away the substrate.
COLOUR/PIGMENT FILLING IN THE PORES
After colouring, anodised aluminium has a characteristic “metallic” look. This is caused because of the roughness left after a uniform electro-chemical etching. The deeper the pores, the rougher the surface will be but the colours will also be that much more durable.
Technique of colour anodising
There are several techniques for colour anodising aluminium. One technique is electrolytic colouring, which involves immersing the anodised aluminium in an inorganic metal salt bath. An electric current is applied to this bath as the metal salts oxidise in the aluminium’s pores. Depending on the chemical conditions of the bath and the length of time immersed, the aluminium colour will vary. Popular anodised colour finishes include gold, black, stainless, clear, brown, bronze, and nickel.
Advantages of aluminium anodising
Anodised aluminium possesses a lot of advantages over any other type of coatings. What is unique, is that no additional layer is applied to the aluminium during anodising. Anodising creates a layer that is built up from the existing aluminium. The oxide layer is fully integrated into the material.
a) Appearance of aluminium anodising
Anodising protects the natural feel and appearance of aluminium with its aesthetically pleasing looks. Anodised look feels better than a painted artificial look.
b) Resistance to corrosion & wear
Anodising increases corrosion resistance and the material retains its appearance for a longer period. Anodising creates a hard, wear-resistant layer which protects the underlying aluminium. Anodised aluminium is used in high traffic areas subjected to excessive wear and abrasion. It can also be used in areas exposed to sunlight, humidity, heat, etc without any effect on the coating.
c) Increase life span of aluminium anodising
Anodising is a very old and proven process. Anodised materials have a greater life span when compared with any other coating material.
d) Adhesion
Unlike paints and powder coatings, anodising is not a coating. Hence it may not fade or peel off when exposed to atmospheric conditions like sunlight, heat, moisture, etc.
e) Abrasion resistant
The aluminium oxide layer is one of the hardest material next to diamond. The anodic layer is capable of withstanding wear and abrasion in transportation, handling, and fabrication. Powder coatings are not as harder as anodised aluminium.
f) Environmental Friendly and VOC s
The process of anodising aluminium is an environmentally friendly metal coating technique. It does not emit any volatile organic compounds. (VOC s). The waste of aluminium anodising constitutes aluminium sulphate and aluminium hydroxide which are recycled and used in water treatment systems and cosmetics. Anodised aluminium can be used in green buildings.
Anodised Aluminium used for Green Building
g) Surface finish
Anodising creates a uniform and regular finish. The problem of orange peeling and high coating thickness may not occur in anodising. Anodising can be applied to modified materials also.
h) 100% Recyclable
Anodised Aluminium can be recycled and reused to any extend. The recycled product possesses the same quality as the virgin product. Coating removal is not necessary before recycling like other coating products.
i) Filiform corrosion
The diminishing of the internal layer between the aluminium surface and the coating doesn’t happen in anodising like other coatings.
J) Chalking
Chalking is the formation of fine powder on the surfaces of paint films due to weathering, whereas in aluminium no chalking will be formed. The colour , gloss, texture etc shall be retained in all atmospheric conditions.
Aluminium anodising – Applications
Anodised aluminium is used in a lot of applications.
a) Building and construction sector in the form or extrusions which are fabricated and erected for sky light,facades, green building, handrails,doors and windows etc.
b) Used for automobile, boat and aircraft parts
c) Food processing industry
d) Decorative works
e) Marine – Yacht masts, pontoons and decks etc
AIRCRAFT PARTS
Demerits of Anodised aluminium
Aluminium anodising got limited colour selection because of the chemicals used in the anodising process. The available colours may not match with the colour scheme of structures.
Touch-up, repair and re coating of anodised product is not possible.
Anodising is vulnerable to lime and cement, Industrial acid, alkali pollutants etc. Anodised aluminium has to be protected while using in under construction buildings.
Anodising is costly than the other polyester coatings.
Anodising does not cover the welded joints.
Shade variation between batches usually happens in anodising.
The Properties of Aluminium play an important role in its transformation to one of the most significant and versatile materials on earth. The properties of aluminium are acquired from its ability to form aluminium alloys on combining with chemical elements. These aluminium alloys got unique properties that can be customised for various applications. Aluminium sections are available in various forms that include aluminium square bars, aluminium plates, aluminium extrusions etc.
What is aluminium?
Aluminium is a silvery-white lightweight material that makes up for more than 8% of the earth’s core mass. It is the 13th element of the periodic table. and is the third common element on earth other than silicon and oxygen. Aluminum is available in the form of aluminium sulphates.
ALUMINIUM PROCESSED IN SMELTERS
Manufacturing process of aluminium
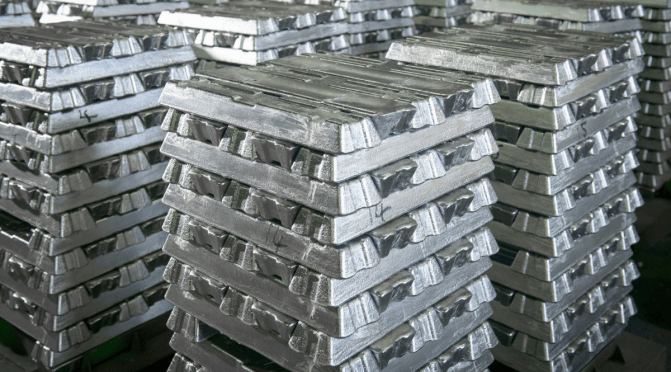
The primary raw material used for producing aluminium is Bauxite. Extracting a tonne of aluminium requires 5-6 tonnes of bauxite. Aluminum is manufactured in two phases: the Bayer process of refining the bauxite ore to produce aluminium oxide. Aluminium oxide is processed in smelters to produce aluminium. The process of extraction of aluminium from bauxite is known as electrolysis or electrolytic reduction.
ALUMINIUM SMELTER
Properties of aluminium.
Aluminum is one of the most commonly used building material. Aluminum is the preferred choice for a lot of applications because of its unique and valuable properties.
a) Light weight properties of aluminium
Aluminium is lightweight and is 1/3rd the weight of steel and is one of the lightest materials in the world. Even though aluminium is lightweight it is very strong and corrosion-resistant. Because of its lightweight properties, aluminium can reduce the dead loads on a structure and optimise the design. This optimisation can reduce costs in a lot of applications.
b) Corrosion Resistant properties of aluminium
Aluminum is corrosion-resistant, due to the formation of a thin oxide film on its surface. This film acts as a barrier and prevents corrosion.
c) Non magnetic properties of aluminium
Aluminum is non-magnetic and a very good conductor of heat and electricity. Because of these properties aluminium is used for power transmission cables, computer components, LED lights, etc
d) Flexibility in moulding and fabricating
Aluminum is processed in both cold and hot conditions. It can be easily pulled, moulded, rolled, and extruded very easily. Similarly, aluminium can be formed into thin sheets of even 4-micron thickness. They can be welded and fabricated to any shape. Aluminum is used for making sophisticated aircraft parts to foils for wrapping. Considering the flexibility of fabrication into any shape aluminium forms an integral part of the construction sector for facades, skylights, green building structures, doors, and windows, etc
ALUMINIUM GLASS HOUSE
e) Aluminium alloys
Aluminum forms a huge variety of alloys in combination with a lot of chemical elements. Even the smallest change in the percentage of ingredients can change the metal properties. This gives the much-needed flexibility for usage in various conditions. Aluminum zinc alloy is used for making computer and mobile components, similarly aluminium with silicon is used for manufacturing alloy wheels and automobile components. A small percentage of elements can vary the properties to any extend.
f) No toxic and odourless
Aluminum is non-toxic and orders less. Hence it is used extensively in the food processing and beverage industries.
g) Strength at low temperatures
Aluminum can retain its strength even at very low temperatures wherein steel tends to get brittle in low temperatures.
h) Coating/painting
Aluminium can be coated/finished using any colour in line with the objects colour scheme.
i) Recyclable
Aluminum is a hundred percent recyclable. The recycled product has all the qualities of a virgin product.
j) Reflective properties of aluminium
Aluminum posses very good reflectivity. Hence it is used for roofing sheets and Light shades. Aluminum roofing can reflect heat and cools the ambient temperature.
Applications of aluminium in construction sector
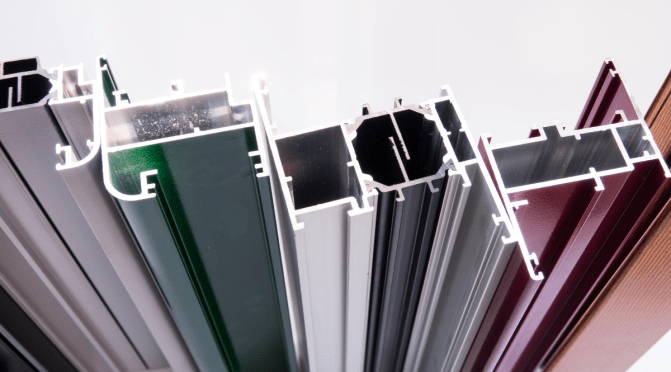
Aluminum can be welded, fabricated, painted, and moulded into any shape and forms. They are lightweight and can be lifted and erected very easily. Because of these unique qualities, aluminium is one of the most versatile, significant, and cost-effective materials used in the construction sector. The most important use of aluminium is in the form of extrusions. Aluminium is also available in form of aluminium square bars, aluminium plates etc. Extrusions are fabricated/jointed to form doors, windows, and partitions, frames of facades, skylight structures, green buildings, aluminium structures, etc. Aluminum extrusions are coated/painted to match the colour scheme of the building/structure. Because of these qualities, aluminium is the most popular material used extensively in the construction sector.
ALUMINIUM EXTRUSIONS FOR VARIOUS USES
Aluminium coatings
Aluminum itself is non-corrosive due to the formation of thin oxide films on the surface for protection from corrosion. Then why you need a coating for aluminum.
a) Enhance the look and appearance
Mill finished aluminium is dull in colour and may not always match with the building/structure’s colour scheme. On the application of the coating, the aluminium structures can match the colour scheme of buildings/structures. Designers/architects proposes the type of coating and colour to be applied after analysing the utilities, environment, and colour schemes. A coating matching with an appropriate colour scheme can enhance the appearance and look of structures/buildings.
b) Increase the Corrosion resistant properties
Most of the cases the oxide film on the surface of aluminium is sufficient to take care of corrosion. In some cases, the structures need an extra protection from corrosion. Similarly long exposure to moisture and water can damage the natural oxide film. The coatings can increase the thickness of oxide film and can provide an extra layer of protection which in turn enhance the protection against wear and tear, handling defects, and corrosion.
ALUMINIUM CLADDING
c) Hardness of members
Coatings can increase the hardness of the materials and protect the material from excessive wear and abrasion encountered on transportation, loading, fabrication erection, etc. Coatings also protect the structures against possible wear and abrasion when used in high traffic areas.
d) Dye marks
Mill finished aluminium have dye marks. Coatings cover these dye marks and makes the surface look smooth and even.
e) Reflectivity
Coatings increase the reflectivity of aluminium and hence used for roofing sheets and light covers.
ALUMINIUM CLADDING
Coatings and treatments on aluminium
The most commonly used types of coatings are as follows. The type of coating basically depends on the choice of colour, hardness required, durability and area of application. The following are the the three different types of coatings commonly used for aluminium.
<p value="Balancing rafts or floating rafts are used when the bearing capacity of the soil is very low. This <a rel="noreferrer noopener" href="https://vincivilworld.com/2020/05/25/foundation-types-shallow-and-deep-foundations/" target="_blank">foundationBalancing rafts or floating rafts are used when the bearing capacity of the soil is very low. This foundation protects against soil settlements and works on the principle that the total weight of the soil and water excavated for the foundation equals to the total load of the proposed structure. They are called zero settlement structures and are used for high rise towers with multiple basements. This type of foundation is preferred only when the soil is very compressive and soft and even friction piles are not able to support the loads.
The basic concept of a floating raft is countering the weight of excavated soil and water with the total load of the structure resting over it. ie. The same weight of excavated materials is replaced by a structure with the same weight. Because of these balancing floating rafts are also known as balancing raft foundations or compensated foundation. The vertical pressure at the foundation depth remains same before and after excavation.
Advertisements
Concerns of Floating Raft/Balancing Raft
Execution of a floating foundation demands massive earthwork excavation in high water table areas. Open dewatering may not be sufficient to control a large amount of water flowing in the excavated areas. Wellpoint dewatering systems have to be run simultaneously with the excavation to lower the water table.
Excavation of floating foundations can trigger soil collapse and soil scoring from the bottom of existing foundations. Sheet piles have to be erected to protect the building against any possible damage during excavation.
Materials required for temporary retaining walls like sandbags, PCC blocks, etc has to be organised and mobilised before starting excavation. Temporary retaining walls have to be constructed in tandem with excavation works.
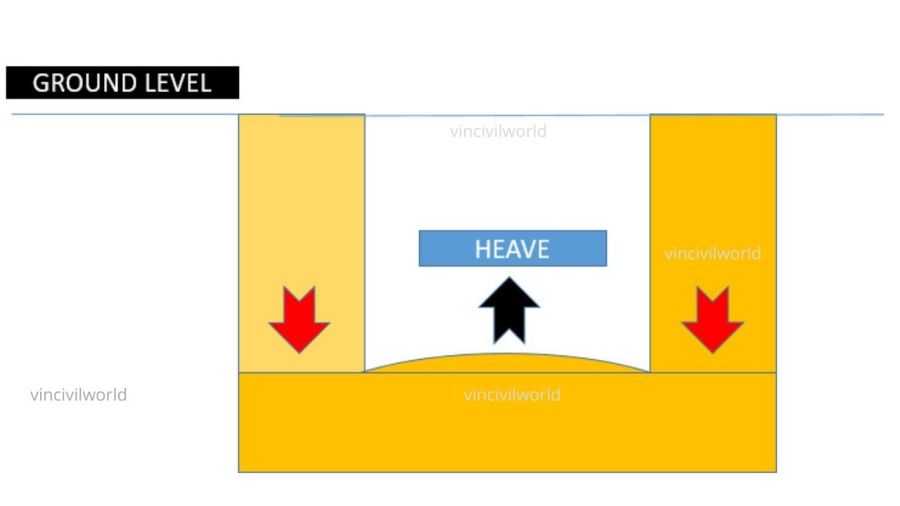
Heave formation in Floating Raft Foundation
Heave formation can always happen while doing deep excavations because of the weight of soil on both sides of the excavation pit. Heaves formations cannot be avoided in any case but have to be controlled or else it may initiate foundation settlements. Heave formation can be minimised by further lowering the water table to a depth below the founding level of the structure. Installation of friction piles or micro piles on partially completed excavation surfaces can also control heave formation to an extent. Concrete bands are provided at the bottom level to control heave formation.
Balancing raft foundations are adopted for high rise buildings with multiple basements. Execution of these foundations requires highly skilled professionals and micro-level supervision supported by an experienced and skilled workforce. All safety precautions have to be done to protect the nearby structures from any damage.
Cement is considered as the most significant substance used in construction which acts as a binder which can adheres the materials together. Cement is a hydraulic binder when mixed with water and sand transforms into mortar and when mixed with water and aggregates converts to concrete which can be used for a number of applications. As per World cement association concrete comes second only to water as the most used resource. China is the largest producer of cement with 53% and India follows with 8% with this production likely to be doubled in next ten years.
The basic raw materials used for cement manufacturing is lime stone or chalk and shale or clay. Cement clinkerisation plants are normally located near the raw materials areas and most of the the times the plants are equipped with conveyors which can directly feed the raw materials from the mines
Based on the technic adopted for mixing raw materials the manufacturing process is divided into wet process and dry process. Wet process is normally used now a days. But dry process is also gaining popularity due to their energy efficiency and when the ingredients are hard.
WET PROCESS OF CEMENT MANUFACTURING
The wet process of cement manufacturing is divided into a number of stages
a) Raw material extraction
b) Grinding
c) Proportioning and mixing and preparing composition based on the raw material purity.
e) Preheating the composition
f) Burning the composition in a kiln to form clinkers
g) Clinker cooling with gypsum addition and grounding to fine powder.
h) Storing in silos and packing and loading for conveying.
The raw materials needed for cement manufacturing are
a) CALCAREOUS (i.e. chalk consists of limestone.) b) ARGILLACEOUS (i.e. clay consists of silicates of alumina.)
a) RAW MATERIAL EXTRACTION
Major raw material involved in the cement manufacturing process is limestone. Cement manufacturing plants are located near the limestone sources for easy access to the raw materials or else it turnout to be expensive to transport the materials from outside. The next major ingredient is clay which have to be located around 25-30 km within the plant premises to minimise the cost incurred in transportation.
Lime stone obtained from open cast mines are transported and feeded to a limestone crusher and clay is placed in a clay crushers. Other raw material like sand which controls the kiln temperature and iron ore etc can be transported or supplied from outside sources.
b) RAW MATERIAL GRINDING
The raw materials calcareous (lime) extracted are crushed to make a size of 6 inch and further crushed to make it 3 inch in secondary crushers. The argillaceous materials (clay) are washed to remove the organic contents and stored in basins and limestone is stored in silos.
c) PROPORTIONING MIXING AND PREPARATION OF COMPOSITION
The washed Clay and crushed lime stone are conveyed and mixed in desired proportion and further grinded in a wet grinding mill where both the materials are closely mixed in the presence of water to form a slurry .The slurry is stored in storage tanks where minor corrections in the compositions are carried out. The slurry which constitutes around 35-40% water is constantly kept in agitation to prevent the settling of limestone and clay.
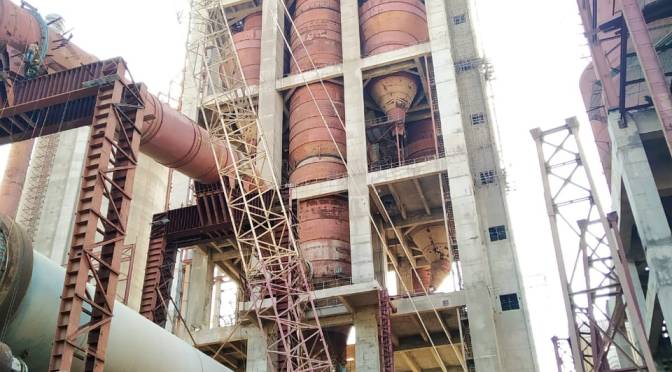
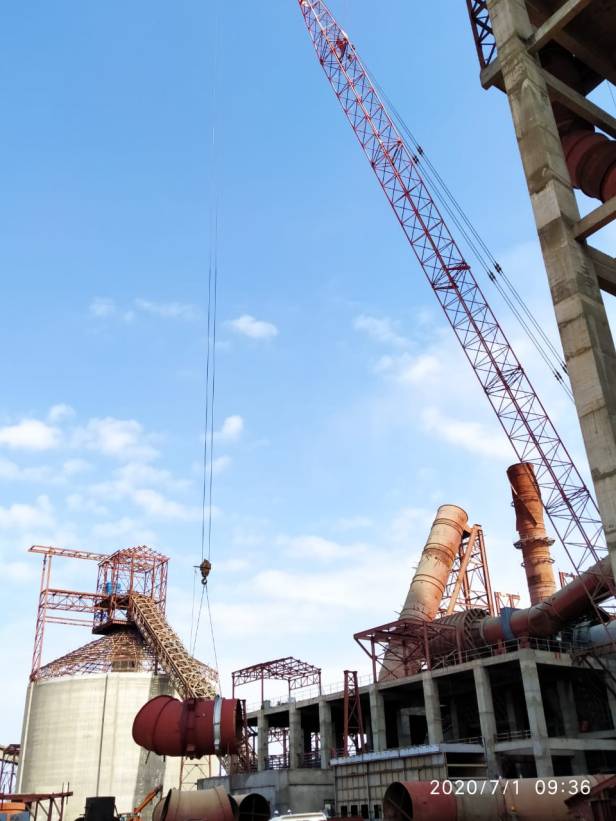
The preheaters are used to heat the raw mix and drive off carbon dioxide and water before it is fed into the kiln.The raw meal passes down the preheater tower while hot gases rise up, heating the raw meal. At the entry point of kiln the raw meal largely decarbonates .
e) BURNING OF COMPOSITION IN KILNS
The decarbonated slurry is fed directly to an inclined steel cylinder which is called rotary kiln .In the rotary kiln through a series of reactions clinker is produced. The kiln is made of a steel casing lined with refractory bricks which have to withstand the reactions happening inside the kiln. The kiln is divided into three zones depending on the process happening in each zone and the temperature at each zone. The kiln is heated from the bottom using coal, oil or gases.
In the first zone water and moisture from the decarbonated slurry is evaporated at a temperature of 400C and the process is known as drying zone.
In the second part which is the calcination zone temperature is around 1000 degree and carbon dioxide is removed and is immediately converted into flakes after loosing the moisture. These flakes or modules are taken into the third stage with the help of rotary movement of the kiln.
In the third stage which is called the burning zone or clinkering zone and the temperature their will be around 1300-1500 degree . In this zone the lime and clay reacts to produce calcium aluminates and calcium silicates. Immediately on entering the burning zone aluminates and calcium silicates get fused and the modules are converted into a dark greenish balls and is called clinker. The size of the clinker ranges from 5 mm to 20 mm. These are the chemical reactions happening in the kiln.
F) CLINKER COOLING WITH GYPSUM ADDITION AND GROUNDING TO FINE POWDER
The cooled clinkers are finally grinded in ball mills. At this stage gypsum(2-4%) is added which functions to reduce the setting time of cement. The grinded powder is take to the cement silos for storage. The particle distribution is also done in a graded manner. The stored grinded powder is taken to the packing plant and packed for distribution
ALSO READ : DRY PROCESS OF MANUFACTURING OF CEMENT
ALSO READ : DIFFERENCE BETWEEN DRY PROCESS AND WET PROCESS OF MANUFACTURING.